Pneumatic vs. Electric Case Erectors: Air Consumption, Energy Cost and Accuracy at 40 CPM
Pneumatic and electric case erectors look interchangeable on a quotation sheet, and for a single-machine line running one shift they often are. The difference becomes a hard engineering and financial decision the moment you run 40 cases per minute across two or three shifts, or the moment your electricity price rises above a threshold most plants crossed years ago. This article replaces the slogan “electric is greener” with the numbers that actually drive the choice: real compressed-air cost, the power each drive draws at line speed, and the forming accuracy each control method can hold.
The short version is that pneumatics win on capital cost and simplicity for low-duty lines, while servo-electric drives win on energy, accuracy and repeatability for continuous 24/7 duty. The crossover is not vague — it sits at a calculable air consumption and a calculable annual running hour count, and both are given below so you can place your own line on the right side.
The Short Answer
Take a standard FEFCO 0201 box in single-wall B-flute board, 400 x 300 x 250 mm, run at 40 CPM (cases per minute). A pneumatic erector of that duty draws 400 to 800 L/min of free air and, once you account for how compressors actually make that air, that is equivalent to 2.5 to 4.5 kW of electrical load on the supply. A servo-electric erector covering the same box and speed draws 1.8 to 3.0 kW at the motor, with no compressed-air load at all.
The gap is not the compressor’s fault alone. Generating compressed air is one of the least efficient operations in a plant: every Nm³ (normal cubic metre) of air costs 0.10 to 0.12 kWh of electricity to produce, and because the whole air system operates at only 10 to 15 per cent overall efficiency, one useful kWh of pneumatic work actually consumes 6 to 8 kWh at the meter. That ratio — not the nameplate of the erector — is what makes pneumatics expensive to run.
Two practical consequences follow. Below roughly 2,000 running hours per year, the pneumatic machine’s lower purchase price and near-zero drive maintenance usually beat the servo’s energy saving. Above that, and especially above 4,000 hours per year on two or three shifts, the servo’s lower draw and tighter control recover its premium inside the first two years. For lines in regions where industrial electricity exceeds 0.15 USD per kWh, the crossover moves earlier still.
What Compressed Air Really Costs
The compressor is the hidden second motor on every pneumatic line, and almost nobody meters it. A reciprocating or rotary-screw unit does not deliver one kWh of pneumatic energy for one kWh of electricity; it delivers one after losing most of the input to heat, pressure drop and leakage.
Where the 6-to-8 ratio comes from
The figure is well established in plant engineering. Producing 1 Nm³ of compressed air needs about 0.10 to 0.12 kWh at the motor. But the air system as a whole — compressor, after-cooler, dryer, distribution and the inevitable leaks — runs at 10 to 15 per cent overall efficiency. Divide one useful kWh by that efficiency and you get 6 to 8 kWh drawn from the supply for every kWh of actual pneumatic work performed at the tool.
That matters because an erector’s pneumatic actuators are almost never the only load. The same line usually feeds the vacuum generator for blank pick-up, the flap folders and the case pusher. A realistic pneumatic erector at 40 CPM therefore pulls 400 to 800 L/min of free air, and at the supply that is 2.5 to 4.5 kW of metered electricity before you add the vacuum pump.
Leakage is the silent tax
A single 3 mm orifice at 6 bar bleeds roughly 100 L/min continuously, day and night, whether the machine is running or not. Most pneumatic erector lines carry several such leaks at fittings, seals and quick couplers. Halving them is often worth more than the entire debate between drive types, which is why the maintenance rhythm below starts with the air system rather than the machine.
Pneumatic vs. Electric: The Energy Numbers
The comparison below is the working envelope we size a line against. Speeds, pressures and power are typical values for a single-lane erector on an FEFCO 0201 case; your board grade will move the grammage and therefore the sealing load, but the drive draw is set by motion, not by glue.
| Drive | Air consumption | Supply power at 40 CPM | Control repeatability | Typical purchase premium |
|---|---|---|---|---|
| Pneumatic (air cylinder) | 400 – 800 L/min | 2.5 – 4.5 kW equivalent | ±2 to 3 mm | Baseline |
| Servo-electric | 0 L/min (own vacuum option) | 1.8 – 3.0 kW | ±0.3 to 0.5 mm | +20 to 35 per cent |
The annual difference is easy to model once you know the air draw and the running hours. Use this arithmetic directly:
Annual energy cost = air consumption (L/min) × 60 × annual running hours ÷ 1000 × 0.11 kWh per Nm³ × electricity price per kWh

Example: 600 L/min × 60 × 4000 h ÷ 1000 × 0.11 × 0.16 USD
        = 600 × 60 × 4000 = 144,000,000
        ÷ 1000 = 144,000
        × 0.11 = 15,840 kWh
        × 0.16 USD = 2,534 USD per year (pneumatic air alone)

Servo equivalent at 2.4 kW × 4000 h × 0.16 USD = 1,536 USD per year
Annual saving = 998 USD, before maintenance and leakage
At the example load the pneumatic air alone costs about 2,534 USD per year, while the servo’s whole electrical draw is about 1,536 USD — a 998 USD annual gap before you count the vacuum pump, dryer power and leakage that pneumatics also carry. Over a 2,000 to 8,000 hour year the gap scales linearly, and on a three-shift pharmaceutical or food line it routinely exceeds 2,500 USD per machine per year.
Board Grade Sets the Sealing Load
Drive choice is independent of board, but the case the drive has to form is not. The values below are the working envelope we size vacuum, compression and glue grammage against, and they decide how much motion the erector must perform regardless of its drive.
| Board | Nominal thickness | Wall count | Liner grammage | Glue (bottom, 0201) |
|---|---|---|---|---|
| E-flute, single wall | 1.6 mm | 1 | 90 – 120 g/m² | 0.5 – 0.8 g |
| B-flute, single wall | 3.2 mm | 1 | 110 – 150 g/m² | 0.7 – 1.0 g |
| C-flute, single wall | 4.0 mm | 1 | 120 – 170 g/m² | 0.9 – 1.2 g |
| BC double wall | 7.0 mm | 2 | 150 – 200 g/m² | 1.4 – 1.8 g |
| AB double wall | 8.0 – 9.0 mm | 2 | 170 – 200 g/m² | 1.6 – 2.2 g |
Single-wall E and B grades are the friendly case for any drive: low crushing risk, short open time, modest grammage. Double-wall BC and AB grades demand longer compression and more glue, and the heavier blank places more load on the vacuum generator and the folder — which is precisely where a pneumatic cylinder, drifting with line pressure, starts to lose squareness late in a shift.
Accuracy, Squareness and Changeover
Energy is only half the story. The other is what the box looks like when it leaves the machine, and how reliably it looks the same after a changeover.
Why ±2 to 3 mm matters
A pneumatic cylinder stops where the air pressure, the load and the seal friction happen to put it. Across a shift, with the compressor cycling and the line voltage wandering, the stopping point of a folder or mandrel drifts by ±2 to 3 mm. On an FEFCO 0201 that is enough to push the panel angle off and to leave the case visibly out of square — a defect measured as squareness, the perpendicularity of the case walls. Cases that fail squareness stack poorly, jam in the downstream case sealer, and read as “cheap” on a retail shelf.
A servo-electric axis, by contrast, is closed-loop on position. It holds the folder or mandrel to ±0.3 to 0.5 mm regardless of load or supply pressure, because the drive is correcting every millisecond. The case leaves square every time, and the measurement that matters — the diagonal difference across the case mouth — stays inside tolerance.
Changeover repeatability
This is where the accuracy gap turns into labour. A pneumatic changeover means re-setting mechanical stops, air-pressure regulators and dwell timers by hand, then running cases and adjusting until squareness passes. A servo changeover is a stored recipe: the PLC moves each axis to its taught position to ±0.3 to 0.5 mm the instant the recipe loads. For plants running more than a few stock keeping units, that difference is the difference between a 5-minute and a 25-minute changeover, repeated several times a day. If your mix is wide, the servo pays for itself on changeover time alone; if you run one box size forever, pneumatics lose nothing here.
Noise, Heat and the Cleanroom Question
The two drives also change the room. A pneumatic erector exhausts air constantly, and each exhaust is a small bang; an open line of cylinders runs in the 78 to 85 dB(A) band, often above the level that requires hearing protection over a shift. The servo-electric line is dominated by the conveyor and the vacuum pump and typically sits 10 to 15 dB(A) quieter.
Heat is the subtler effect. A compressor making 600 L/min rejects its wasted energy as heat right next to the line, and in a poorly ventilated hall that can lift the local temperature by several degrees in summer — which then makes the operators open doors, which then defeats the dust control. The servo puts almost none of its loss into the room air.
Cleanroom suitability follows directly. In a cleanroom (ISO Class 7 or 8), pneumatic exhaust throws oil mist and particles into the classified space, and the dryer and oil-water separator become contamination sources you have to manage. A servo-electric erector with an integral or decoupled vacuum option emits no exhaust into the room, which is why pharmaceutical and electronics lines in classified spaces almost always specify servo drives.
Maintenance: What Each Drive Demands
The running cost is not only energy; it is the hours you spend keeping the machine alive. The two drives ask for different routines, and both are listed below as a rhythm rather than a table.
Every shift: drain the compressor receiver and check the line pressure gauge; on the pneumatic machine verify the air preparation unit is not past its bowl level; on the servo machine confirm the HMI shows no axis temperature alarm.
Every week: blow down the air line filter and inspect the bowl for oil-water accumulation; on pneumatics, check cylinder rod seals for weeping; on servo, verify the reducer lubricant level and listen for bearing noise.
Every month: replace or clean the main line filter element; test the dryer dew point; on servo, re-torque the coupling and check the encoder cable for chafing; on pneumatics, swap any actuator that shows slow stroke.
Every quarter: service the compressor intake filter and check belt tension; on pneumatics, rebuild or replace the most-cycled cylinders and their seals; on servo, back up the recipe parameters and run a squareness audit on a reference case.
Every year: calibrate the pressure transducers and the servo position datum; drain and refill the reducer oil; replace the dryer desiccant. A pneumatic line that follows this rhythm typically holds 95 to 97 per cent uptime; a servo line following the same discipline reaches 98 to 99 per cent, mostly because it has fewer seals to fail.
PLC Alarms You Will Actually See
Both drives speak through the PLC. The messages below cover the bulk of unplanned stops on either architecture, and the first checks are the ones a competent operator should run before calling maintenance.
| Alarm | Meaning | First three checks |
|---|---|---|
E-12 Vacuum Low |
Blank pick-up pressure below setpoint | Suction cup wear, filter condition, pump relief valve |
E-18 Air Pressure Drop |
Line pressure below 5.5 bar at actuator | Compressor load, line leak, regulator setting |
E-27 Servo Follower Error |
Axis deviation beyond 1.5 mm from command | Belt tension, encoder coupling, squareness datum |
E-33 Drive Over-Temp |
Servo amplifier above 75 °C | Cooling fan, reducer lubrication, duty cycle |
Note that E-18 Air Pressure Drop is specific to pneumatics — when it appears the fault is almost always upstream of the machine, in the compressor or a leaking coupler, not in the erector itself. On servo lines the equivalent message is E-33 Drive Over-Temp, which usually means the reducer is starving for oil or the duty cycle has crept above the rated profile.
Choosing for Your Line
The decision collapses to three variables: annual running hours, the number of box sizes, and your electricity price. The guidance below is a rhythm of thresholds, not a table.
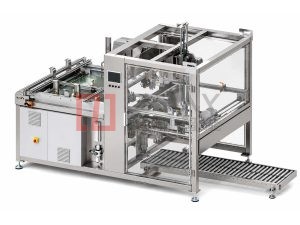
If you run below 2,000 hours per year on a single box size, choose pneumatics. The capital saving and the simple, seal-and-go maintenance beat the servo’s energy edge, and the accuracy penalty does not show up on a uniform load. A single-lane Single-Piece Carton Erector in pneumatic form is the standard fit here, and the simpler drive also shortens any retrofit or relocation.
If you run two or three shifts (4,000-plus hours), or your electricity price is above 0.15 USD per kWh, choose servo-electric. The math above already recovers the purchase premium inside two years, and the accuracy and quiet operation are bonuses you did not pay extra for. For high-volume duty the two-lane output of our Double-Head High-Speed Case Former is the configuration we recommend, with servo axes on every folder.
If your line is in a cleanroom (ISO Class 7 or 8) or packs pharmaceutical or electronics product, choose servo-electric on contamination grounds alone — the exhaust-free room is a compliance requirement, not a preference. Where you run more than 200 stock keeping units in small batches, the servo recipe changeover is what protects your uptime; a pneumatic line spending its day re-setting stops will not keep pace. Multi-piece and tray formats follow a different logic and are covered by our Three-Piece Carton Erector; sizing and board-grade questions are answered in our FAQ.
FAQ
Is electric always cheaper to run?
On energy, yes — typically 30 to 45 per cent less at the meter for the same box and speed, because it avoids the 6-to-8 kWh penalty of making compressed air. On total cost, only once running hours clear roughly 2,000 per year and the purchase premium is amortised.
Can a pneumatic machine be converted to servo?
Not economically. The frame, vacuum and control architecture differ; a true conversion is a new machine. What is worth doing is adding a servo axis to one critical folder to recover squareness while keeping the rest pneumatic.
Why does my pneumatic line fail squareness late in a shift?
Compressor cycling drops line pressure, the cylinders slow and the folder stops short. Check E-18 Air Pressure Drop, fix the leak, and if the problem persists through the shift, the servo upgrade is the real answer.
Do I need a dryer for pneumatics?
Yes. Without a dryer the dew point climbs, water reaches the seals, and you get freeze-ups in winter and sticky valves in summer. The dryer and oil-water separator are not optional on a pneumatic erector.
Ready to cut your cost per case? Send your carton specifications — length, width, height, flute grade, target cases per minute and annual running hours — to [email protected] or WhatsApp +86 13681839278. Our engineers will return an energy-and-accuracy model and a machine sizing sheet within 24 hours, with no obligation.
Want To Know More About Our Upgraded Machines?
Send your carton specifications and output demand, our engineer will provide free technical scheme & quotation
Latest Products
Subscribe To Get Latest News & Technical Guides
Leave your business email to receive free industry articles and new product updates