Erecting Low-Grade and Thin Corrugated Board: Settings for Recycled and Lightweight Grades Below 1.5 mm
Thin board is not a defect. It is a deliberate cost decision that saves 12 to 20 per cent on blank spend, and it is being adopted across retail packaging, e-commerce mailers and light industrial shipping. The problem is that most case erectors in service were specified and set up for B-flute at 3.2 mm and C-flute at 4.0 mm, and they are then asked to run E-flute at 1.6 mm or a lightweight recycled grade at 1.1 to 1.4 mm. The machine does not fail loudly. It produces double feeds, cup marks, bulging cases and adhesive joints that open within a day.
This article covers the measurable properties that separate a workable lightweight grade from an unworkable one, the failure modes each produces, and the specific settings that have to change on the machine when you switch grades down.
Why this is a settings problem, and only sometimes a board problem
The instinct when thin board misbehaves is to call the board supplier. That is sometimes correct — a grade below about 90 g/m² liner weight with an RCT under 3.0 kN/m will not hold a formed case regardless of machine settings. But in most cases the board is within its own specification and the machine is simply outside its adjustment envelope for that grade.
There is a fast way to separate the two. Take ten blanks from the incoming pallet, form them by hand to the correct geometry, fill each with a representative load, and let them stand for one hour at production ambient conditions. If the cases stay square, stay erect and show no bottom bulge, the board is serviceable and the machine is the variable. If they bulge at the sides or the bottom flaps separate at the score, the grade is below what the application needs and no amount of machine tuning will recover it.
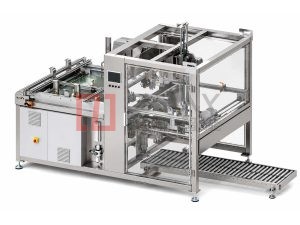
Where the application is a single grade at high volume, the single-piece case erector is the machine architecture that handles it most efficiently, because a fixed-format machine can be set up precisely for one grade and left there. The adjustment-heavy work described below applies where grades change.
Run this test before touching a single setting. It costs an hour and prevents weeks of iterative adjustment against a problem the machine cannot solve.
The measurable properties that matter
Four numbers determine whether a grade will run, and only the first is usually quoted by suppliers.
| Property | Workable range | Marginal | Will not run reliably |
|---|---|---|---|
| Liner weight, kraft or test liner | 125 g/m² and above | 100 to 125 g/m² | Below 90 g/m² |
| Caliper, single wall | 1.6 to 3.2 mm | 1.3 to 1.6 mm | Below 1.1 mm |
| Ring crush (RCT), cross direction | Above 4.0 kN/m | 3.0 to 4.0 kN/m | Below 3.0 kN/m |
| Moisture content at machine | 6 to 9 per cent | 9 to 11 per cent | Above 12 per cent |
Caliper is the number that gets attention because it is easy to measure with a micrometer, but RCT is the number that predicts failure. A 1.4 mm blank with good liners and an RCT of 4.5 kN/m will form and hold. A 1.9 mm blank made from heavily recycled liner with an RCT of 2.6 kN/m will collapse under its own load within minutes of forming, and it will feel stiffer in the hand than the first sample while doing so.
Moisture interacts with both. Board above 11 per cent moisture loses roughly a third of its compression strength and becomes plastic under the fold rails; board below 6 per cent cracks along the score line. The window is narrower on thin grades than on heavy ones, which is why a humidity logger at the machine is worth more here than on a B-flute line.
Failure modes and what each one points to
Six failures account for almost all thin-board problems on a case erector, and each has a different correction.
Double feeds. Two blanks leave the magazine together. On thin board this is almost always a vacuum set too high rather than too low — the cup pulls the second blank through because the first blank flexes and the air path is not sealed. Reduce vacuum, do not increase it.
Cup witness marks on the printed face. The cup has deformed the liner permanently. Reduce cup diameter and vacuum, and switch to a cup with a softer lip. Where the print is high-value, specify soft bellows cups at the enquiry stage; a standard nitrile cup will mark lightweight coated board at any vacuum that reliably picks it up.
Flaps that spring back after folding. The fold rails are not holding the flap long enough for the adhesive to set. On thin board the flap has less mass and less stored energy, so it returns before the compression section takes it. Extend compression time or add a hold-down rail.
Adhesive strike-through. Glue has penetrated to the printed face. This is a bead volume and open time problem, not a glue problem. Reduce bead volume and shorten open time.
Bottom bulge under load. The formed case is square on the discharge but bulges within minutes of loading. This points to RCT, not to the machine. Verify with the hand-forming test above.
Joints that open within 24 hours. The bond formed at the line but failed on setting. On absorbent recycled board the adhesive is drawn into the liner before it can develop tack. See the adhesive section below.
The settings that have to change
When moving from B-flute at 3.2 mm to a lightweight grade at 1.4 mm, the following adjustments are the ones that matter. They are listed in the order they should be made, because each one affects the next.
- Vacuum: reduce from a typical 0.5 bar to 0.35 to 0.45 bar. Lower is better provided the blank still picks up; on thin coated stock it is not unusual to run as low as 0.30 bar.
- Cup set: reduce cup diameter by one size and increase cup count if the blank is wide or flexible. Distribution matters more than total area — four small cups across the width outperform two large cups at the edges.
- Feed roller pressure: reduce by roughly 15 to 20 per cent. Excessive pressure on thin board deforms the leading edge, which then catches on the magazine lip and produces the intermittent feed jams that look like a magazine problem.
- Fold rail clearance: increase by 0.3 to 0.5 mm. Thin board buckles rather than folds if the rails are set to the calliper of a heavier grade.
- Adhesive bead: reduce volume from a typical 1.0 g per case to 0.6 to 0.8 g, but widen the bead slightly and reduce its thickness. A narrow, thick bead on thin board concentrates stress on the liner and is the mechanism behind most strike-through.
- Compression: reduce from 2.5 s to 1.2 to 1.8 s only where the adhesive has been re-selected for the shorter window. Trimming compression without changing adhesive converts a clean joint into an intermittent one.
- Mandrel and fold geometry: verify the fold angle is being achieved by the tooling rather than by the board’s own stiffness. On thin grades the board contributes less to forming, so the machine has to do more of the work.
The single most common mistake is to treat vacuum as a strength setting. On thin board, vacuum should be the lowest value at which pick-up is reliable, and that value is materially lower than operators expect.
Adhesive selection is where most failures actually originate
Recycled and lightweight liners are porous. Standard hot-melt applied at standard bead volume is drawn into the substrate within a fraction of a second and arrives at the compression section with little adhesive remaining at the interface. The bond looks acceptable on the line and opens on setting.
Three corrections apply, in order of preference. First, select an adhesive with a shorter open time and higher viscosity so that less volume is required for the same bond. Second, reduce bead thickness while increasing bead width, which reduces penetration depth for the same contact area. Third, if penetration cannot be controlled, move to a cold glue or starch system that sets by absorption rather than by cooling — this is the standard answer where recycled content is high and the application allows the longer compression times that starch requires.
The field test is the same one used for tape adhesion: seal cases, let them stand 24 hours, then tear the flap open and inspect the bond line. Fibre on both faces indicates a good bond. A clean, glue-starved interface indicates absorption and a change of adhesive grade.
Dust, sensors and the second-order problem
Recycled board sheds. The dust comes off the cut edges and the trim, and it accumulates on anything the air stream touches.
The practical consequences are consistent. Photoelectric sensors used for blank presence, flap detection and case counting lose contrast and start producing spurious alarms that are recorded as machine faults. Adhesive nozzles accumulate a bake-on residue that changes bead geometry gradually, so the failure is a drift rather than an event. Vacuum filters load faster than on virgin board, which reduces vacuum and produces intermittent pick failures.
The corrections are straightforward and should be specified up front rather than discovered. Add extraction at the magazine and the trim area — this is the highest-value single addition for a recycled-board line. Move blank detection from photoelectric to mechanical or inductive where geometry allows. Shorten the vacuum filter service interval from monthly to weekly. And clean nozzle tips on a fixed schedule rather than on a fault, because bake-on residue is easier to remove in thirty seconds than after a line stop.
Vacuum-side maintenance deserves its own routine on a recycled-board line. Cup lips, filter elements and line joints should be inspected every shift for the first month of a new grade, then weekly once the drift pattern is known. The reason is that dust loads the filter gradually and vacuum falls gradually, so the symptom appears as an unexplained intermittent pick failure weeks after the grade change, long after anyone connects it to the board. The service routine for that failure set is set out separately in maintaining vacuum lines and suction cup feeding systems.
When the thin grade is still the right answer
A plant running 1.4 mm board instead of 3.2 mm saves on blank cost, freight and storage. To make that saving real rather than nominal, three conditions need to hold.
The machine must be adjustable across the full grade range with tool-free changeover, because a plant that saves on board and then spends the saving on changeover labour has moved cost rather than removed it. A servo-driven machine with recipe memory holds settings per grade, which is what makes the range practical rather than theoretical — the same requirement that governs multi-size erecting for contract packers.
The range of case sizes must be within the machine envelope. Thin board is often used for small or medium cases, and a machine sized for large cases may not run small ones well, since the fold rails and mandrel have a minimum working size.
And the downstream must tolerate the softer case. A lightweight case that reaches a palletiser at speed, or a stacker that compresses the pallet, may need reduced stack heights or a slower transfer. Board cost savings that are lost to damaged pallets are not savings.
Grade-change procedure: the first thirty cases
Every time the line moves to a thinner or more recycled grade, run this check before accepting the run.
- Form and inspect the first thirty cases. Ten straight off the machine, ten after a ten-minute settle, ten after loading a representative weight.
- Perform a destructive tear test on three of them at the bottom seam. Inspect for fibre transfer.
- Check the discharge squareness with a tape measure across both diagonals of the bottom face. A difference above 2 mm will cause problems downstream.
- Record the vacuum, bead weight and compression time in the setting sheet for that grade. A grade change without a recorded setting is a grade change you will repeat from scratch next time.
The same discipline applies to the magazine and feed geometry. Where the change in caliper is large, verify the magazine side guides and the blank retainer have been re-set rather than left at the previous grade’s position.
FAQ
Can I run 1.1 mm board on a standard erector?
Sometimes, but rarely well. Below about 1.3 mm the magazine and feed geometry of a machine built for B-flute typically cannot be adjusted into range. Verify with the hand-forming test and a trial run before committing a production order.
Why does the same grade run well on one machine and badly on another?
Because the two machines have different vacuum systems, different cup sets and different minimum fold rail clearances. Thin board is unforgiving of a machine running near the edge of its adjustment range.
Is a vacuum pump better than an ejector for thin board?
A pump gives steadier vacuum at low settings, which matters on thin board where the working window is narrow. An ejector is adequate where the grade is consistent and the vacuum requirement is stable.
Does reducing vacuum reduce pick reliability?
It reduces pick force, which is why cup count and distribution have to compensate. More cups at lower vacuum picks a thin blank more reliably than fewer cups at high vacuum, and it marks the board less.
Should I change the adhesive or the machine first?
Change the adhesive first when the failure is an opening joint, and the machine first when the failure is a double feed or a cup mark. The two problems have different causes and are frequently conflated because both appear as “the machine will not run this board”.
How much thinner board can a servo machine handle?
The servo architecture removes the timing limitation, but not the vacuum, cup or rail limitation. It extends the practical range by roughly one grade step, which is often the difference between a workable and an unworkable lightweight programme. The grade-versus-machine questions buyers raise most often are collected in our FAQ.
Thin and recycled board can cut blank cost by a meaningful margin, but only if the machine can be adjusted to suit it. To check whether your case sizes and grades sit inside the adjustment envelope, send the full size range, the board grades and the required case rate to [email protected] or contact us on WhatsApp at +86 13681839278. We will confirm the practical grade range for your specification, the vacuum and cup configuration, and the settings sheet for each grade, so the first production run is the validated one rather than the trial.
Want To Know More About Our Upgraded Machines?
Send your carton specifications and output demand, our engineer will provide free technical scheme & quotation
Latest Products
Subscribe To Get Latest News & Technical Guides
Leave your business email to receive free industry articles and new product updates