Dual-Head Case Erectors: Doubling Output to 70-90 CPM in a Single Station Footprint
There is a specific problem that a dual-head machine solves and that a single-head machine cannot. It is not “we need more speed”. It is “we need roughly double the output and we do not have double the floor” — a constraint that appears in food and beverage lines where the filler is already delivering 80 cases per minute, in e-commerce sortation where the peak is a four-week window, and in plants where the building was laid out for a line that has since been re-rated upwards.
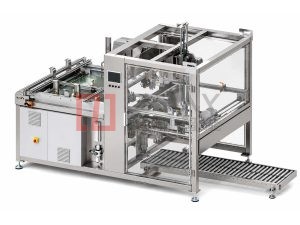
A single-head machine at 35 CPM occupies roughly 6 square metres. Two of them occupy 12. A dual-head machine delivering 70 to 90 CPM occupies 9 to 11 square metres, because the two forming stations share a frame, a vacuum source, a control cabinet and a sealing module. That is a 30 to 40 per cent reduction in floor area per unit of output, and it is the reason the architecture exists.
Two architectures, and they are not the same machine
Dual-head is a category, not a single design. The two common configurations behave differently and suit different plants.
Parallel twin-station mounts two complete forming stations side by side on one frame, feeding one common discharge. Each station runs the full blank-to-formed-case sequence independently; the stations share vacuum, pneumatics, control and sealing. Speed is effectively double a single head, and because the stations are independent, one can be isolated for service while the other runs. This is the configuration that suits single-format, high-volume work, because the changeover is performed twice.
Tandem places two forming points in series along one flow path, so a blank is picked, partially formed at the first point, completed at the second, and sealed once. The cycle time is shortened rather than doubled, which means the mechanism sees higher accelerations at the same output. This is used where the case is large and the forming sequence is long enough that splitting it genuinely saves time, and it is less tolerant of format changes.
The distinction matters at specification time because the service model, the changeover time and the maintenance access requirements are all different. A buyer told “dual head, 80 CPM” without knowing which architecture is being quoted does not yet have enough information to compare two offers.
| Parameter | Parallel twin-station | Tandem |
|---|---|---|
| Output increase over a single head | Close to 2.0 times | 1.5 to 1.8 times |
| Changeover time | Twice a single head | Longer than a single head, sequence re-phasing required |
| Station isolation for service | Possible where specified | Generally not possible |
| Best suited format count | One to two formats | One format |
| Best suited case size | Small to large | Large, long forming sequence |
| Sensitivity to grade variation between stations | Moderate | High |
| Typical installed footprint | 9 to 11 square metres | 8 to 10 square metres |
What sharing components actually changes
The floor saving is the visible benefit. The more consequential effects are the ones that follow from sharing.
Shared vacuum. One vacuum source serves both stations. At 80 CPM the total air demand is high and continuous, so the vacuum system is specified for peak simultaneous demand rather than the duty cycle of a single head. This is where a dual-head machine either works or does not, and it is why compressed air sizing and vacuum maintenance discipline, covered in our support material, become critical rather than optional. A dual head built on an undersized vacuum system will lose pick reliability at rate, and it will do so intermittently, which is the hardest kind of fault to diagnose.
Shared control. One PLC, one HMI, one recipe set. This is a genuine advantage: a format change is entered once and applies to both stations, and the synchronisation between stations is held by the controller rather than by mechanical adjustment. It is also a single point of failure. A PLC fault stops 80 CPM, not 40.
Shared sealing module. One glue or tape module sealing the output of both stations. This is a substantial floor and cost saving, but it means the sealing module runs at twice the cycle rate of a single-head machine. Nozzle wear, blade wear and adhesive delivery all accelerate accordingly. Where the two stations produce cases at a small phase offset, the sealing module sees a more even demand than a single head at the same rate, which is a genuine benefit; where they are synchronised, it does not.
Shared case breakage detection. One rejection station covering both heads. Adequate, but it means a fault on one station can reject good cases from the other unless the controller tracks which head produced each case. Specify head-level traceability, because without it a recurring fault on one station is statistically diluted by the good output of the other and can run for weeks before it is noticed.
The cost structure, stated plainly
The purchase price of a dual-head machine is higher than a single head and lower than two single heads. The per-CPM cost typically falls by 15 to 25 per cent relative to two equivalent single machines, before installation, power distribution, compressed air runs and the floor space itself are counted. Add those and the gap widens considerably, because two machines require two of everything on the plant side.
The counterweight is concentration risk. One line at 80 CPM stops 80 CPM. Two lines at 40 CPM each stop 40. For plants where a stop is measured in minutes of recovered output rather than hours of lost production, the concentration is acceptable. For plants where the erector feeds a line that cannot be buffered, it is the deciding factor, and the correct answer is frequently two single machines or a dual-head machine with single-head isolation so that one station can run while the other is serviced.
Insist on single-head isolation as a specification item. It changes a dual-head machine from an all-or-nothing asset into one that degrades gracefully, and on a 24/7 line that difference pays for itself once.
Synchronisation is the engineering problem
Doubling the number of forming stations doubles the number of things that must agree.
The two stations must deliver formed cases to the transfer with positional agreement of about half a millimetre. Beyond that, a downstream taper, labeller or palletiser pick head begins to fail intermittently, and the failure appears at the downstream machine rather than at the erector. This is why dual-head machines are specified with servo positioning rather than pneumatic actuation on the forming axes: a pneumatic axis returns to a position that depends on the resistance it met, and board grade variation between the two stations then shows up as a positional difference.
Three settings require attention on commissioning and at every grade change.
- Fold rail geometry on both stations must be set to the same dimension, using the same gauge, not set by eye and not set “to match the running station”.
- Vacuum balance between stations must be verified with a gauge at each station, not at the manifold. Unequal vacuum produces unequal pick timing, which produces a station offset that grows with rate.
- Discharge timing must be set so that cases from both stations enter the transfer with consistent spacing. Irregular spacing is the most common cause of transfer jams on a dual-head machine and is often misdiagnosed as a mechanical alignment fault.
Where a dual-head machine is the right answer, and where it is not
Four profiles justify the architecture.
Single format, very high volume. Above roughly 3 million cases per year on one case size, a dual-head machine running one format continuously is the most floor-efficient way to deliver the output. The changeover penalty is paid rarely enough that it does not matter. Below that volume on a single format, a fixed-format single-head machine such as the single-piece case erector covers the requirement at lower capital cost, and the dual-head architecture is buying capacity the plant does not yet have.
E-commerce sortation peaks. Where the peak is measured in weeks rather than days, a dual-head machine covers the peak that a single head cannot, without the changeover penalty of running two independent machines on a shared line. The economics of that peak are discussed in more detail in the fulfilment centre case erecting analysis.
Food and beverage filler lines. A filler at 80 CPM needs an erector at 80 CPM-plus margin. Running two single machines in parallel against a common filler is possible, but the synchronisation burden moves to the line controller and the floor cost remains.
Two-shift or three-shift operations needing redundancy. A dual-head machine with station isolation provides production continuity that two machines cannot match if the plant only has floor space for one.
Three profiles do not justify it.
Many formats with frequent changeover. Changeover is performed per station, so a dual-head machine takes roughly twice as long to change. Where the shift contains six to ten changeovers, the downtime outweighs the throughput, and a single-head machine with fast changeover is the better buy.
Low headroom. A dual-head machine needs adequate clearance for service access above both stations. Below about 2.4 metres of clear height, service access becomes a safety problem rather than a convenience.
Downstream machines that cannot keep up. If the case taper, labeller, checkweigher or palletiser tops out at 45 CPM, a dual-head machine produces a queue, not an output. The erector is rarely the constraint in a line that has not been re-rated as a whole, and buying throughput into a bottleneck simply relocates the constraint.
Maintenance: what doubles and what does not
Wear parts double. Cups, belts, blades, glue nozzles, filters and fold rail inserts all exist twice. Plan the spares inventory on that basis rather than scaling a single-head list.
Scheduled intervention does not double, because the frame, vacuum system and control cabinet are shared. A well-designed dual-head machine has a service load closer to 1.5 times a single head than twice, which is part of where the cost advantage comes from.
What changes most is the diagnostic discipline. On a dual-head machine, a fault on one station can be masked by the output of the other. This is why head-level case counting and head-level rejection traceability are worth specifying: they turn a dilution problem into a visible trend. Where the two stations are instrumented separately for vacuum, servo current and cycle time, a developing fault on one head is visible within a shift. Where they are not, it is visible only when it becomes severe.
Record a baseline for each station separately at commissioning — pick time, fold time, compression time, vacuum at the station, and squareness of output cases. Compare the two stations monthly. Divergence between them is the earliest available signal that something is changing, and it is available before the quality of the output degrades.
| Per-station measurement | Single-head reference | Dual-head target, each station | Investigate when |
|---|---|---|---|
| Vacuum at the station | 0.4 to 0.6 bar | 0.4 to 0.6 bar, matched within 0.05 bar | Station difference above 0.08 bar |
| Pick time | 0.18 to 0.30 s | Same as single head | Drift above 15 per cent |
| Servo forming axis current | Machine baseline | Same, per station | Rising trend above 15 per cent |
| Cycle time deviation | Below 3 per cent | Below 5 per cent | Above 5 per cent |
| Output case squareness | Within 1.5 mm diagonal | Matched between stations | Station difference above 0.5 mm |
| Cases per head per shift | Not applicable | Within 2 per cent of each other | Divergence above 5 per cent |
FAQ
Is a dual-head machine just two machines bolted together?
No, and the difference is the point. A genuine dual-head design shares vacuum, control and sealing, which is what produces the floor and cost saving. Two machines on one frame with separate systems is a different product with a different cost structure.
Can I run one head while servicing the other?
Only if single-head isolation was specified. Ask for it explicitly; it is not universal and it is not always possible on tandem designs.
Does doubling the heads double the CPM?
Not exactly. The output increase is close to double on parallel twin-station machines, and less than double on tandem designs where the forming sequence is split rather than duplicated. Take the rated figure as a starting point and confirm the effective rate at your case size.
Which architecture suits our line?
Parallel twin-station for one or two formats at very high volume; tandem for large cases with long forming sequences. If your shift contains frequent format changes, neither is the right answer and a fast-changeover single head is.
What is the biggest specification mistake?
Under-specifying the vacuum system. A shared vacuum source sized for a single head’s duty cycle will deliver intermittent pick failures at full rate, and that fault will be chased through the forming stations for months before the air supply is suspected.
What should I measure after commissioning?
Vacuum at each station, cycle time for each station, and the squareness of output cases separated by station. Divergence between stations is the signal that matters, and it is only visible if you recorded a baseline for each station in the first place.
If your volume justifies a dual-head machine, the specification decisions that matter are made before the order, not after. Send your case rate, format range, available floor area and clear height to [email protected] or contact us on WhatsApp at +86 13681839278. We will confirm which dual-head architecture fits your line, the single-head isolation provision, the vacuum sizing for simultaneous station demand, and the per-station baseline values to record at commissioning.
Want To Know More About Our Upgraded Machines?
Send your carton specifications and output demand, our engineer will provide free technical scheme & quotation
Latest Products
Subscribe To Get Latest News & Technical Guides
Leave your business email to receive free industry articles and new product updates